Skip to content
+39 0424 85688 info@cidoniostampi.it ISO 9001:2015 · TÜV SÜD
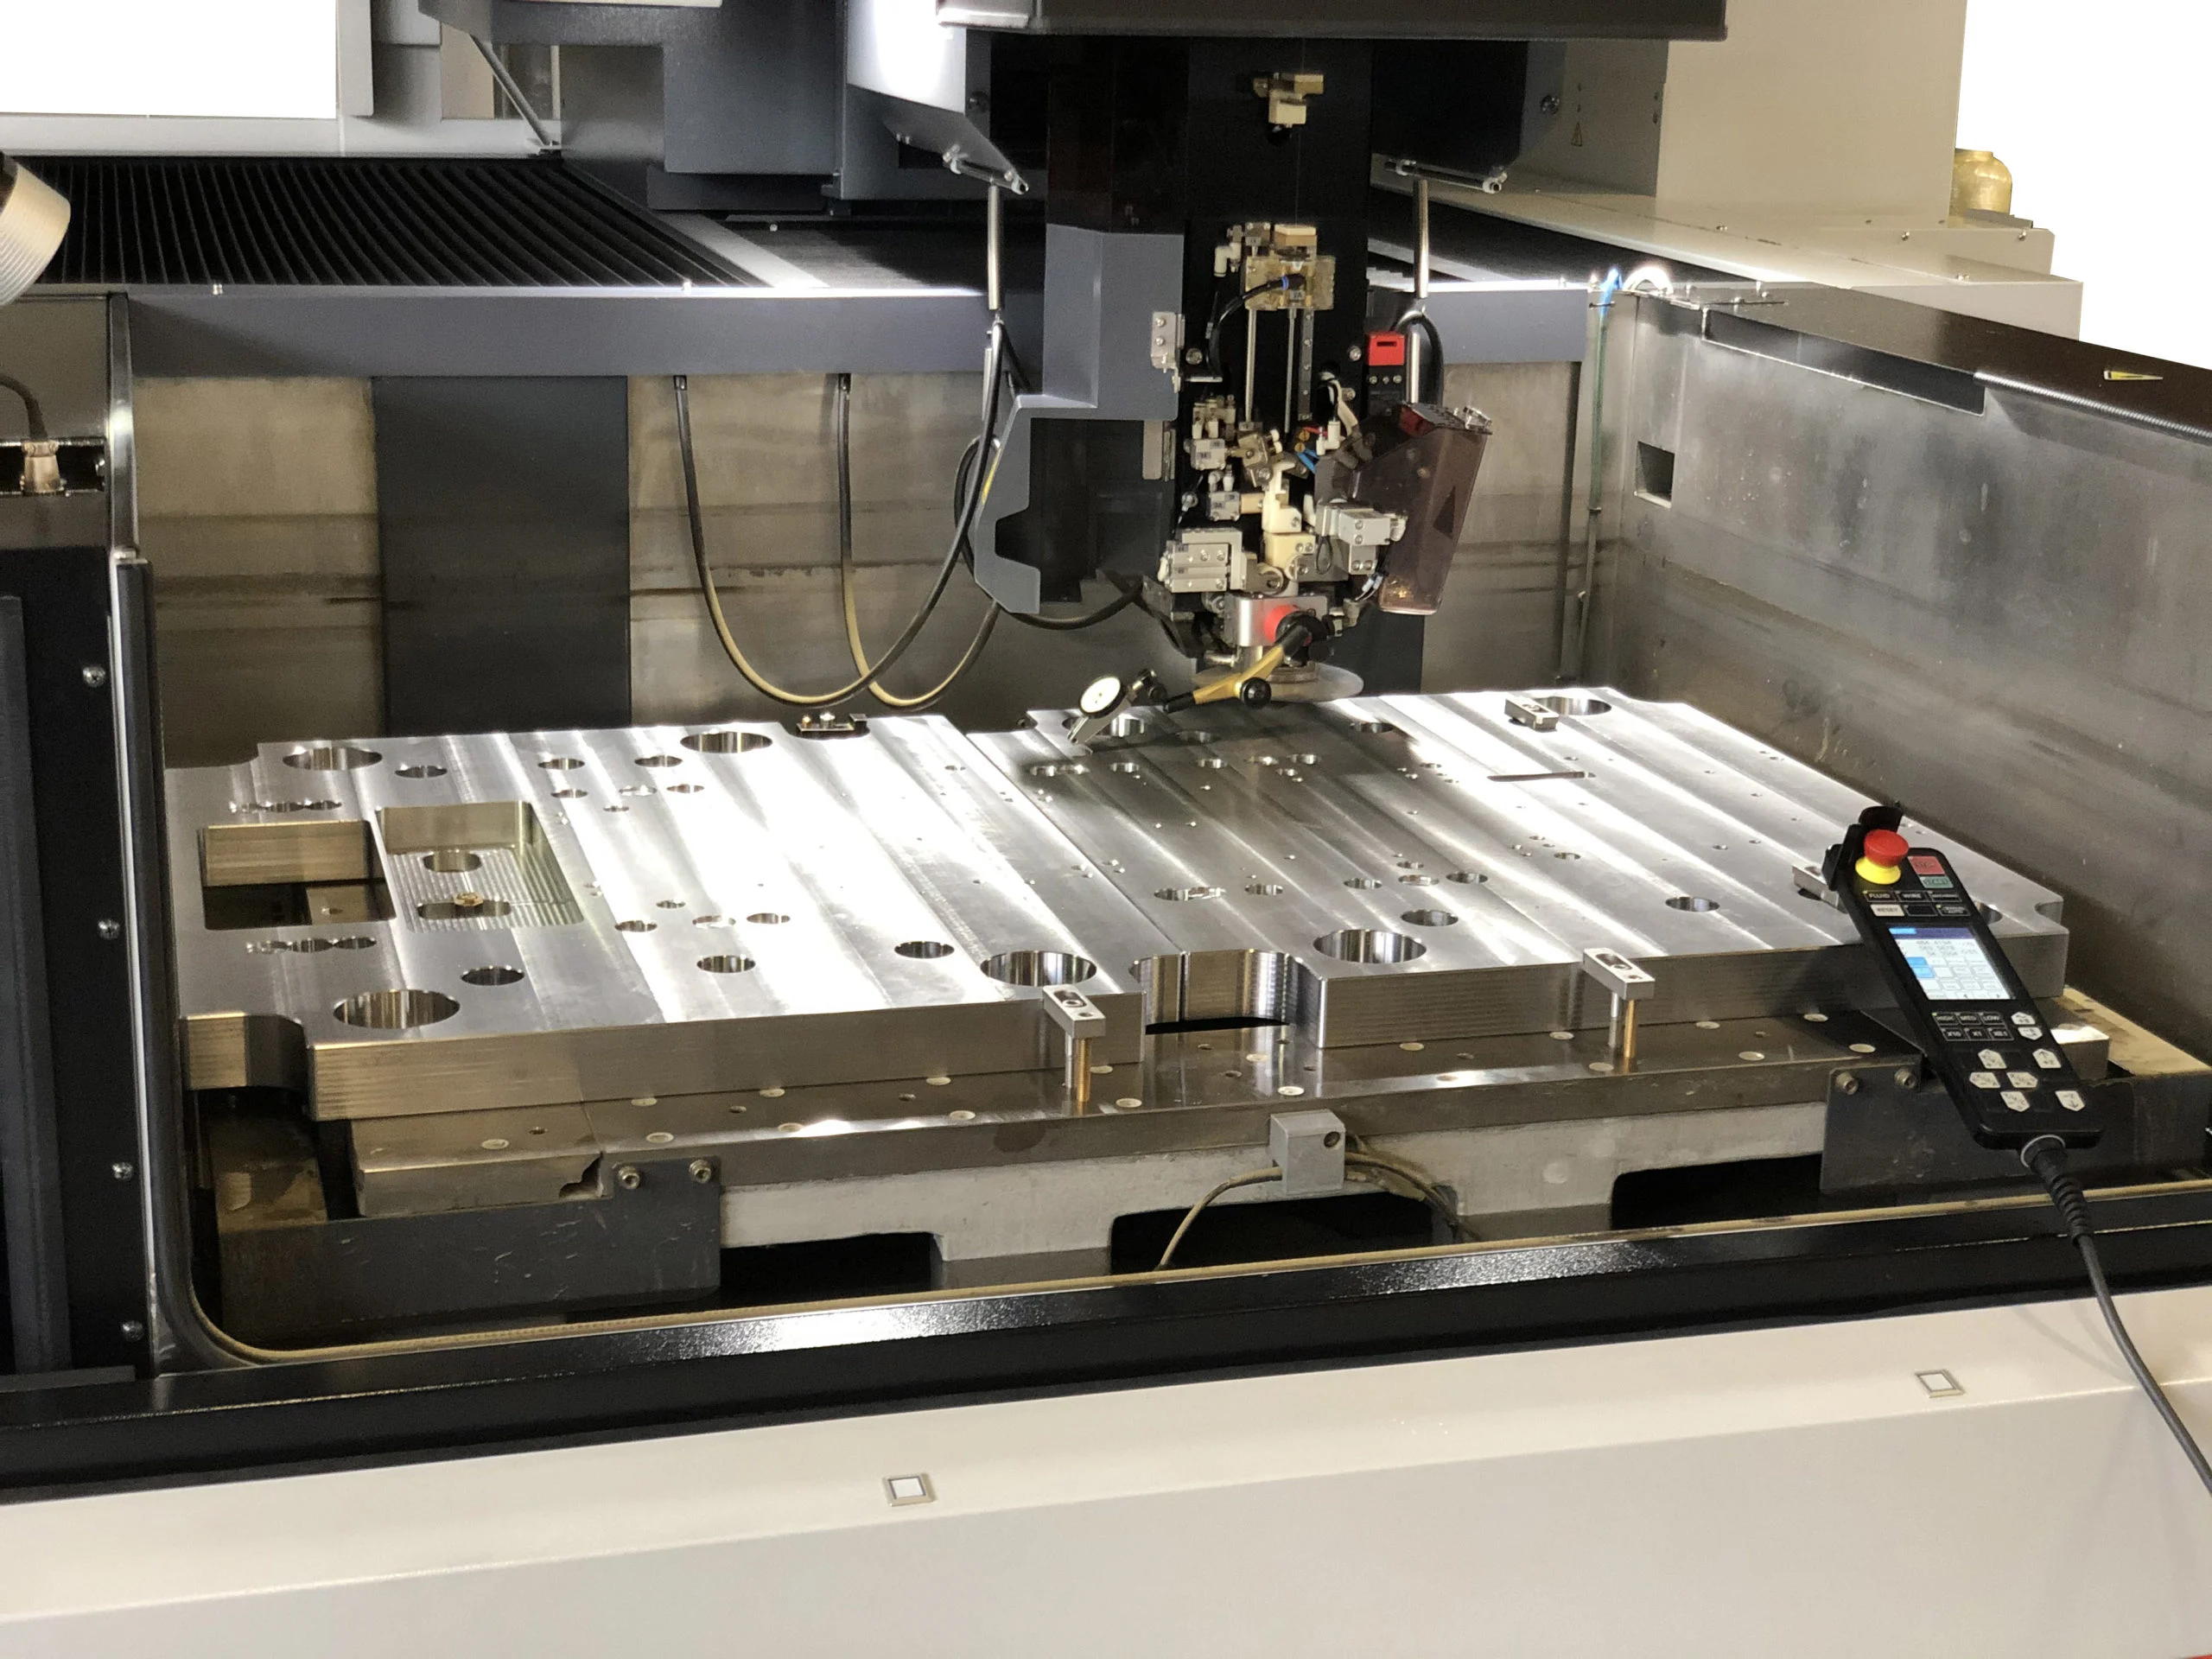
Wire EDM cutting of a die plate

Technical guide

Wire EDM in die construction

Wire EDM cuts hardened materials with extremely high precision and surface finishes down to 0.1–0.2 Ra: this is why it is decisive in building the punches, die inserts and active parts of precision dies.

Quick answer

In brief

Wire EDM cuts hardened materials with extremely high precision and surface finishes down to 0.1–0.2 Ra: this is why it is decisive in building the punches, die inserts and active parts of precision dies.

The Cidonio machine fleet

Machines4 wire EDM machines, submerged and continuous-flush
Maximum travel800 × 600 × 310 mm
Finish0.1–0.2 Ra with superfinishing unit
Latest modelMitsubishi MV4800R

Mistakes to avoid

  • Considering EDM only for difficult parts
  • Ignoring the finish of active parts

How Cidonio Stampi works

Since 1969, we have been designing and building sheet metal dies in Rosà (VI): feasibility study with the customer, 3D CAD design, construction in our own toolroom and tryout with dimensional inspection. UNI EN ISO 9001:2015 certification by TÜV SÜD.

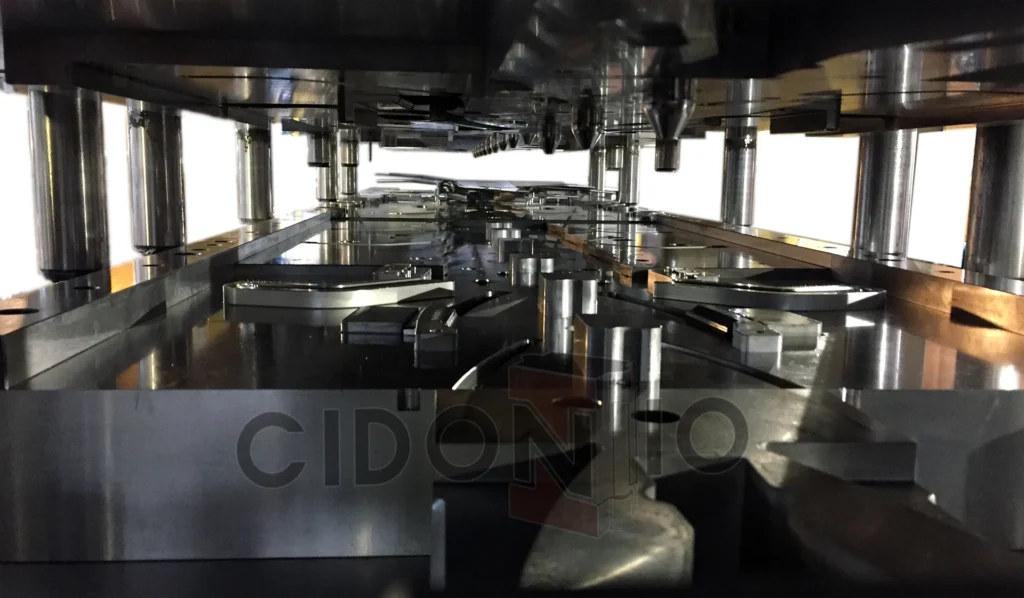
Cidonio Stampi production floor in Rosà, Vicenza (Italy)

FAQs

What is your maximum travel?

800 × 600 × 310 mm.

What finish do you achieve?

Between 0.1 and 0.2 Ra.

Do you have a project?

Send drawings or 3D models: our technical office replies within 24 working hours.

PDF, STEP, IGES, DXF, DWG, ZIP, JPG or PNG – up to 4 files, 20 MB each. Files are used only to assess your request.

Send us your drawing. Technical reply within 24 hours.

Talk directly to the people who design and build your die: no middlemen, reliable lead times and certified quality since 1969.

  • Since 1969
  • ISO 9001 · TÜV SÜD
  • Reply in 24 h
  • Sheet 0.05–12 mm